1 / 1
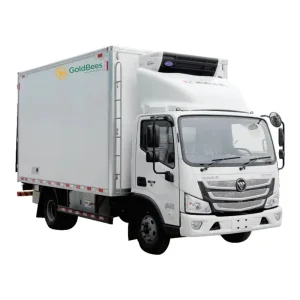
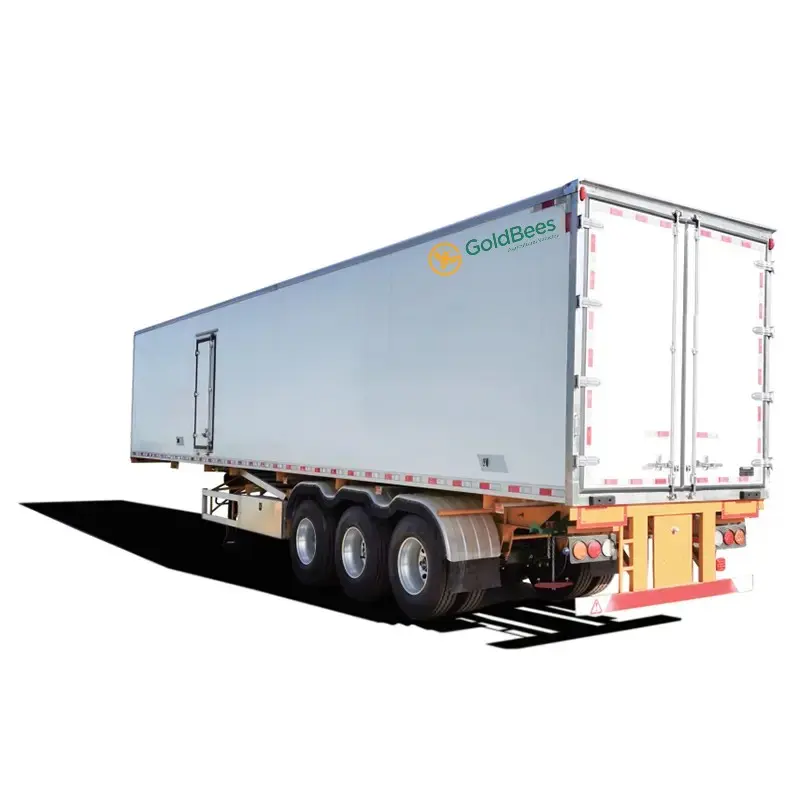
Designed for precision and reliability, this GoldBees refrigerated cold-chain transport semi-trailer integrates cutting-edge technology with robust engineering to deliver unmatched performance in cargo protection, climate control, and operational safety. Ideal for high-value or temperature-sensitive goods, this vehicle redefines modern transportation standards.
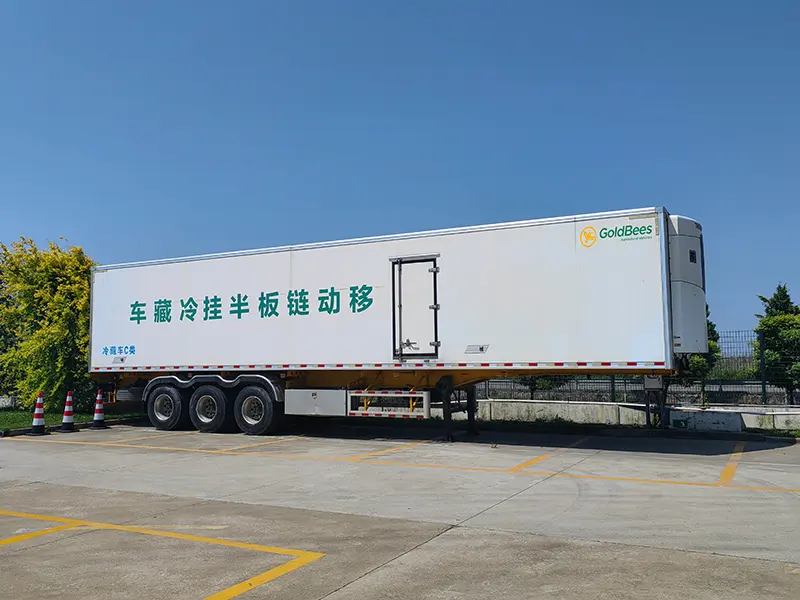
The trailer’s body is constructed with ultra-durable, high-strength materials to ensure secure and damage-free transportation, even under demanding conditions.
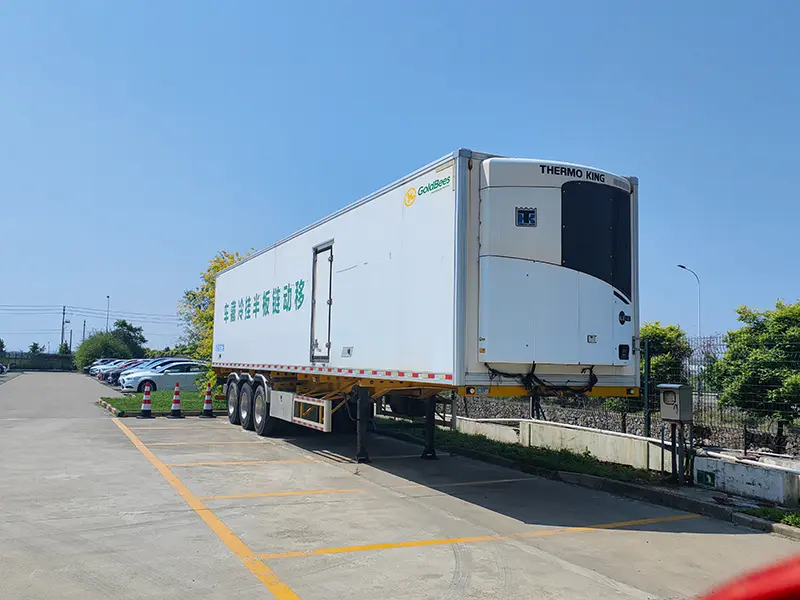
Unique bottom-mounted corrugated ventilation channels, designed in a fortress-style layout, optimize airflow while maintaining stable internal temperatures. This innovation ensures consistent climate control for sensitive cargo.
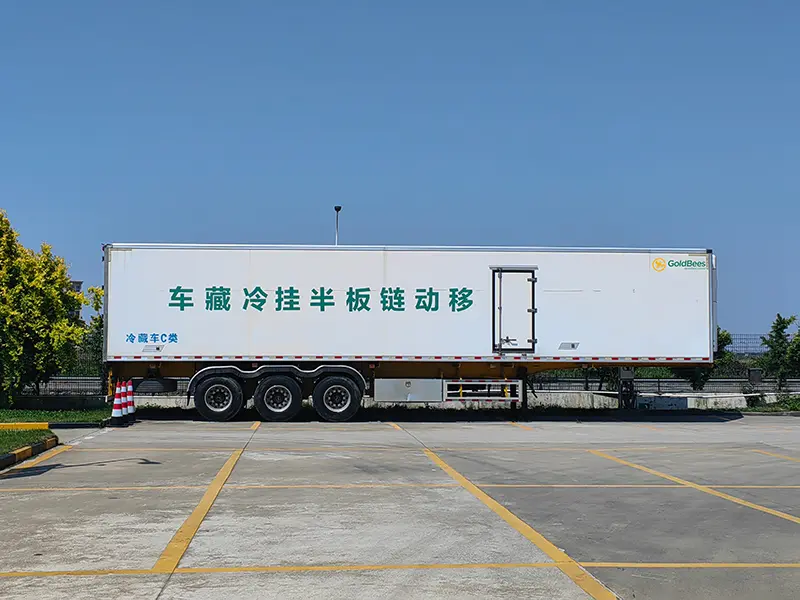
Equipped with a multi-tooth ethylene propylene diene monomer (EPDM) sealing strip on the rear door, the trailer achieves exceptional airtightness, preventing moisture ingress and temperature fluctuations.
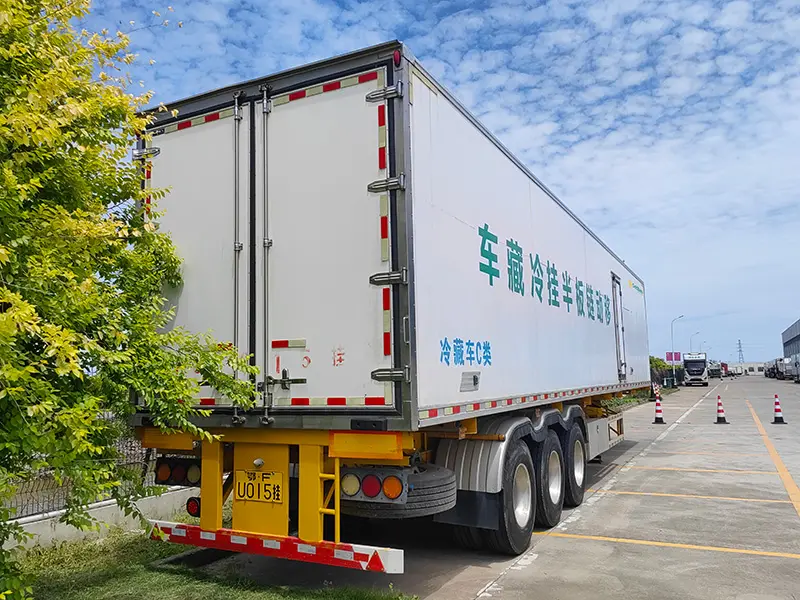
A built-in intelligent monitoring system autonomously analyzes big data, enhancing operational efficiency and safety. Real-time insights help reduce fuel consumption.
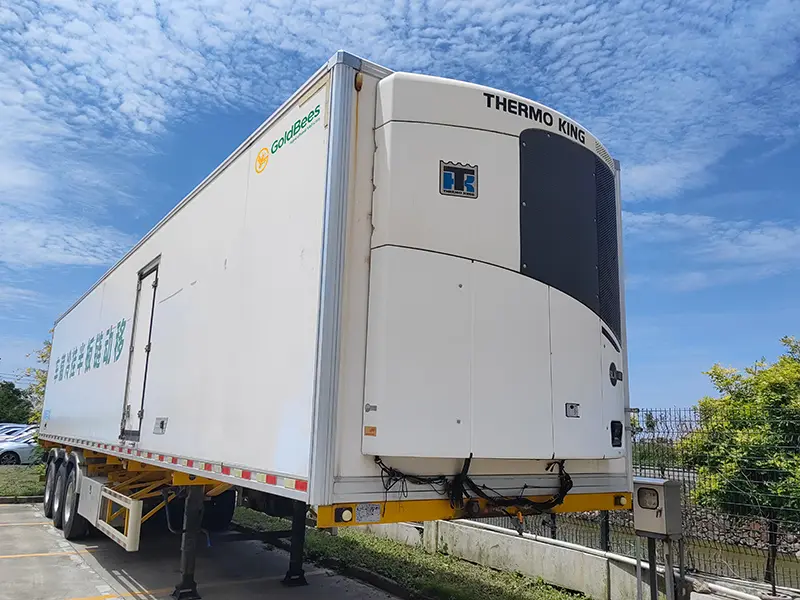
Advanced temperature sensors trigger instant alerts for any deviations from preset thresholds. The system records all incidents, enabling quick troubleshooting and ensuring cargo integrity through actionable data.
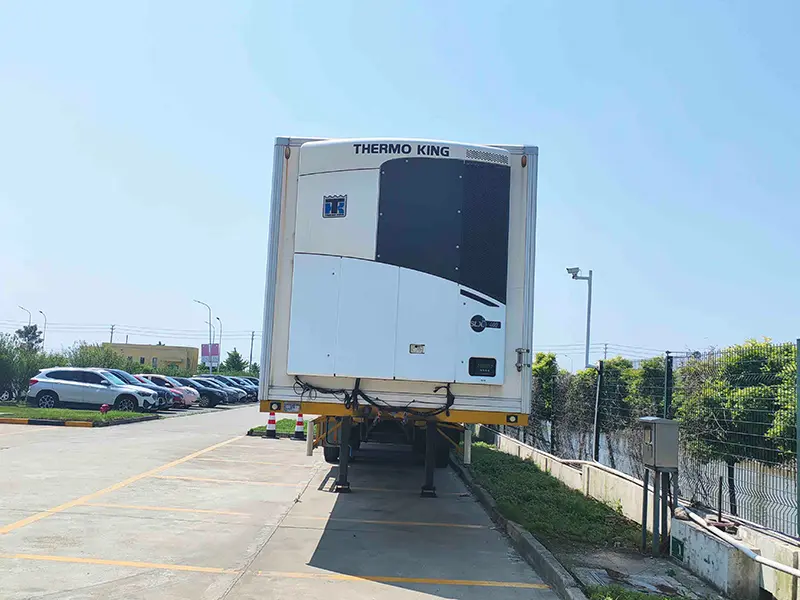
Temperature-sensitive goods (e.g., pharmaceuticals, perishables, fresh vegetables, frozen food & meat, etc.)
High-security logistics (8cm thickness)
Long-haul freight operations (stable temperature control)
Combining rugged durability with smart technology, this high-end cold-chain transport semi-trailer guarantees precision, compliance, and peace of mind. From climate-critical cargo to data-driven fleet management, it is engineered to exceed expectations.
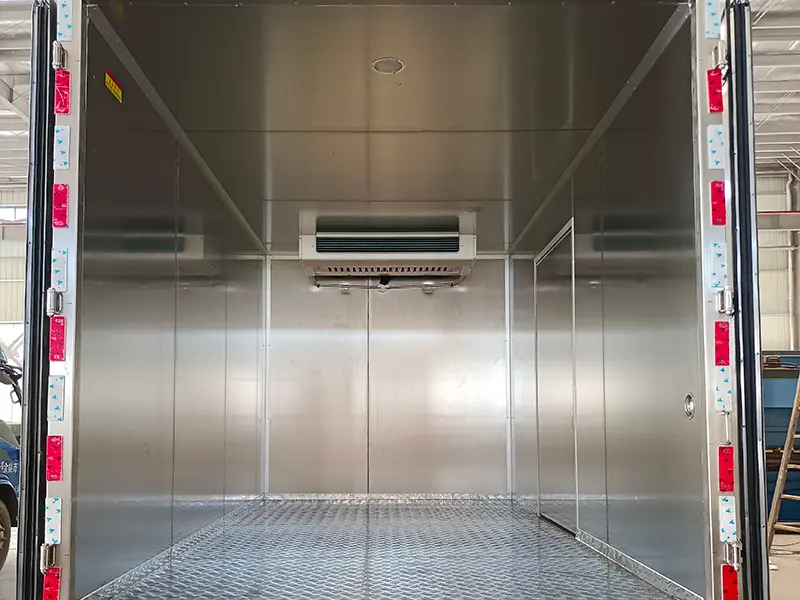
The trailer’s body is constructed with ultra-durable, high-strength materials to ensure secure and damage-free transportation, even under demanding conditions.
Unique bottom-mounted corrugated ventilation channels, designed in a fortress-style layout, optimize airflow while maintaining stable internal temperatures to ensure consistent climate control for sensitive cargo.
Equipped with a multi-tooth ethylene propylene diene monomer (EPDM) sealing strip on the rear door, the trailer achieves exceptional airtightness, preventing moisture ingress and temperature fluctuations.
A built-in intelligent monitoring system autonomously analyzes big data, enhancing operational efficiency and safety while delivering real-time insights that help reduce fuel consumption.
Advanced temperature sensors trigger instant alerts for any deviations from preset thresholds. The system records all incidents, enabling quick troubleshooting and ensuring cargo integrity through actionable data.
It is ideal for temperature-sensitive goods (such as pharmaceuticals, perishables, fresh vegetables, frozen food & meat), high-security logistics (8cm insulation thickness), and long-haul freight operations requiring stable temperature control.